01
Wire shape
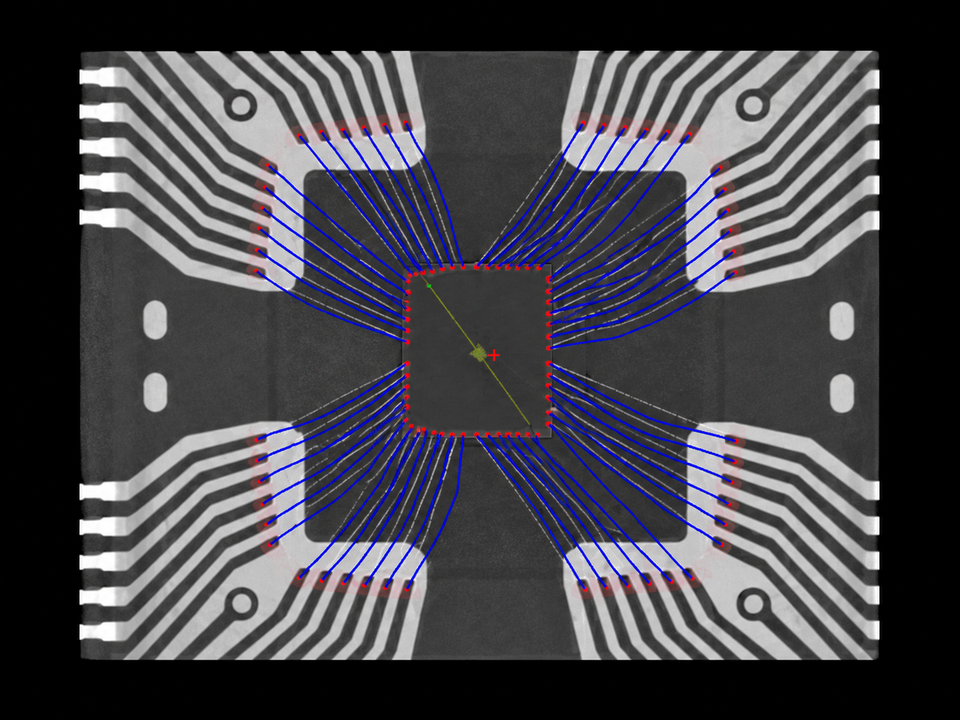
Observe internal wire routing, displacement and deformation, defining reference shapes and inspection regions.
ProductPOST-MOLDING / X-RAY INSPECTION
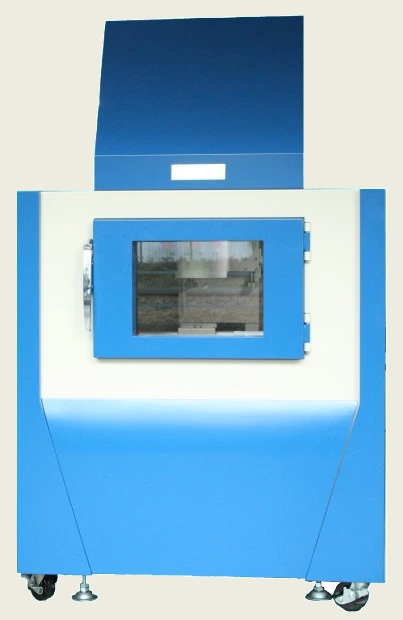
Inspect wires and bond regions concealed by molding with X-ray projections. Build checks around wire shape, continuity and neighboring wires, with feeding, handling and sorting configured for the workpiece.
INSPECTION FOCUS
Define checks from package geometry and actual images. Overlap in a 2D projection does not by itself prove physical wire contact.
Observe internal wire routing, displacement and deformation, defining reference shapes and inspection regions.
Review close wires and projection overlaps, validating viewing directions and decision rules on samples.
Look for unusual interruptions and suspected breaks in wire projections, assessing detectability with actual defect samples.
Define observation regions from the die and leadframe layout to review bond positions and nearby internal structures.
IMAGING & ANALYSIS
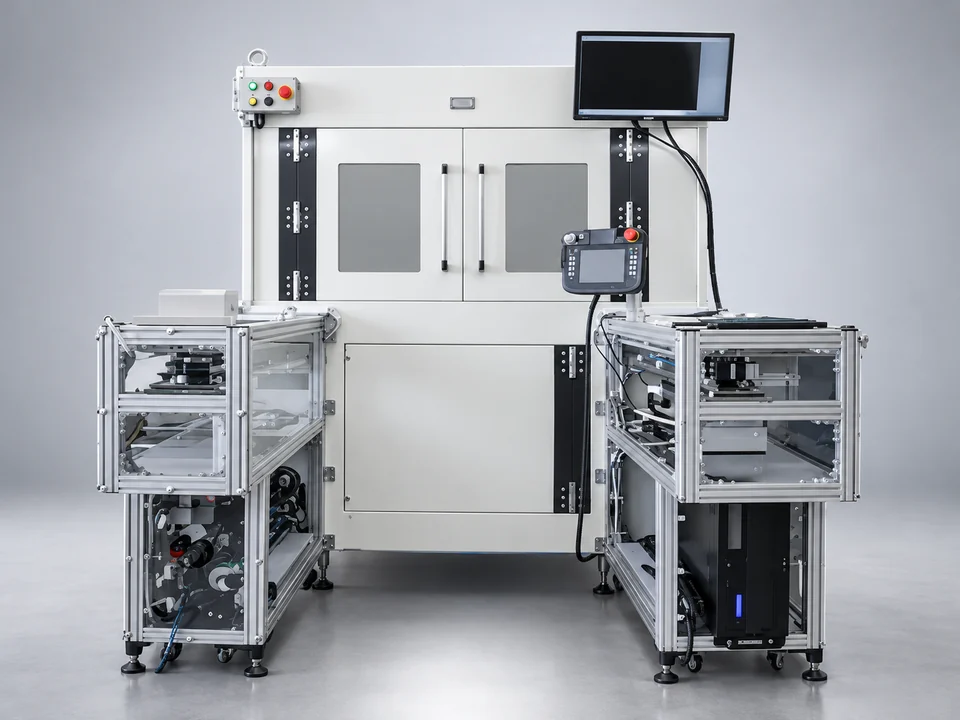
Acquire X-ray projections and organize processing around the actual wire layout. Combine feeding, positioning, imaging and sorting, selecting the configuration for package dimensions, wire materials and line requirements.
SYSTEM CONFIGURATION
Tray, magazine, conveyor or parts feeding, selected for the workpiece.
Options include conveyor, pick-and-place, XY-stage and index handling.
Match the X-ray source and digital detector to package size, materials and observation targets.
Configure marking, sorting, reject discharge or result mapping for the line.
Detectability depends on package materials, wire dimensions, projection direction and imaging conditions. Confirm resolution, cycle time and decision metrics with actual samples and the equipment configuration.
SAMPLE EVALUATION
Describe the package, bump or wire geometry and the inspection questions.
Specify regions, measurements or defect classes and decision conditions.
Review imaging, handling, cycle time and output for an assessable system proposal.
LET'S CONNECT
Get in touch for an initial enquiry, a technical conversation or a discussion of possible solutions.